


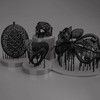
Black Wax Casting Resin
|
Viscosity |
322.4Mpa*s |
|
Tensile Strength |
18.2Mpa |
|
Elongation at Break |
5.13% |
|
Flexural Strength |
21.3Mpa |
|
Flexural Modulus |
385.0Mpa |
|
Bending Strain |
8.90% |
|
Izod Impact-Notched |
9.57KJ/m² |
|
Density |
1.13g/cm³ |
|
Hardness(Shore D) |
65 Shore |
|
Ignition Temperature |
400℃ |
Product Description
This is a very stable and reliable resin, which can be applied to all 3D Plus machines and can also be applied to machines for other manufacturers. It can be used by the engineers, designers and jewelers to directly turn the 3D designs into great jewelry products.
High definition, strength and precision
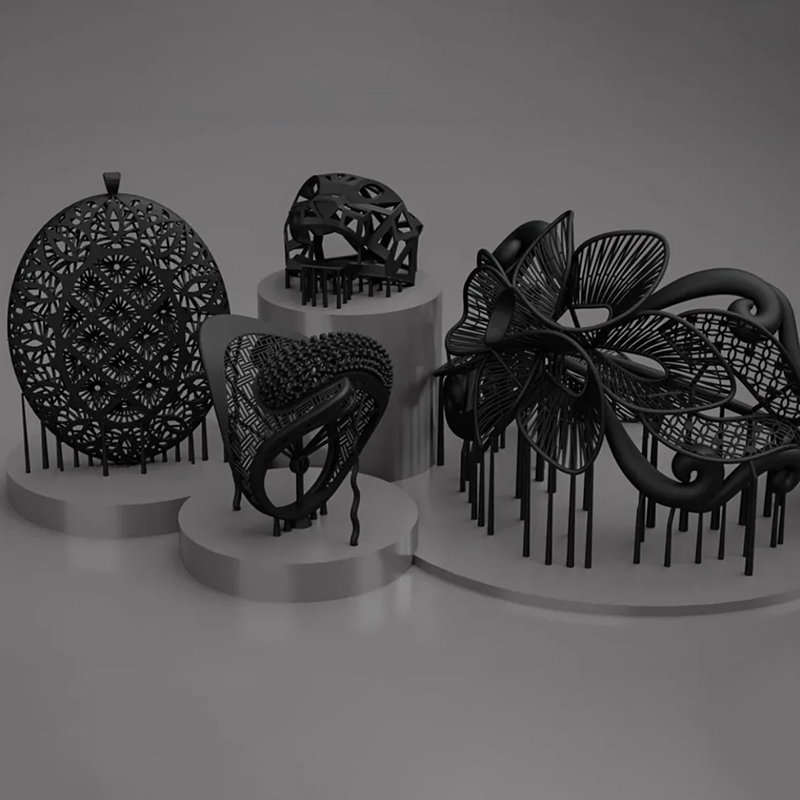
It can capture complicated details and has a strong adaptability, which is an ideal choice to embed gem, and it can also create challenging and unique model.
Smooth surface quality
Before casting, the model printed by the machine has smooth surface, and perfect result can be realized with minimum polishing.
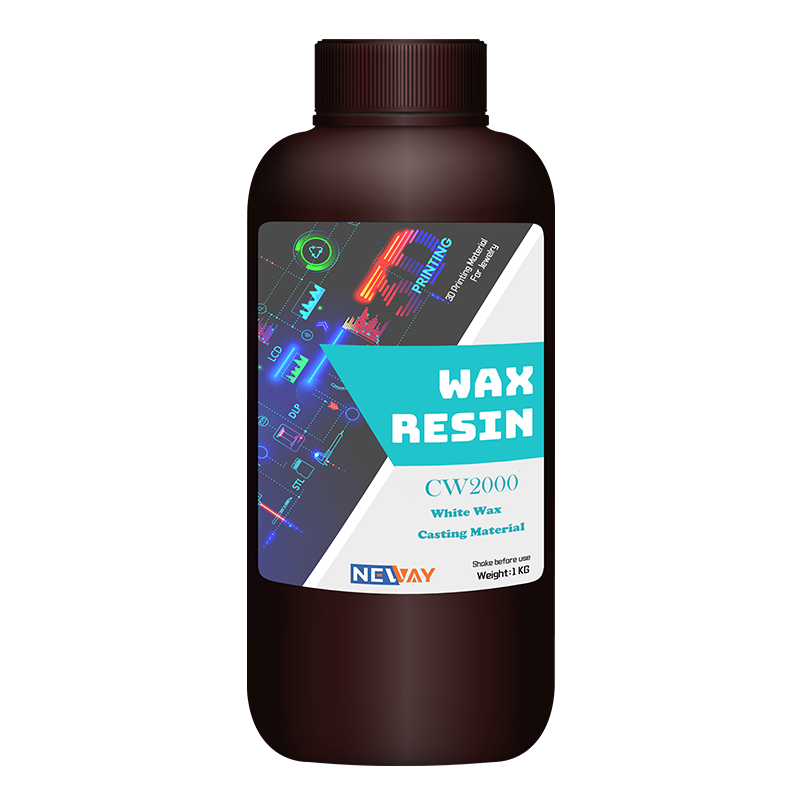
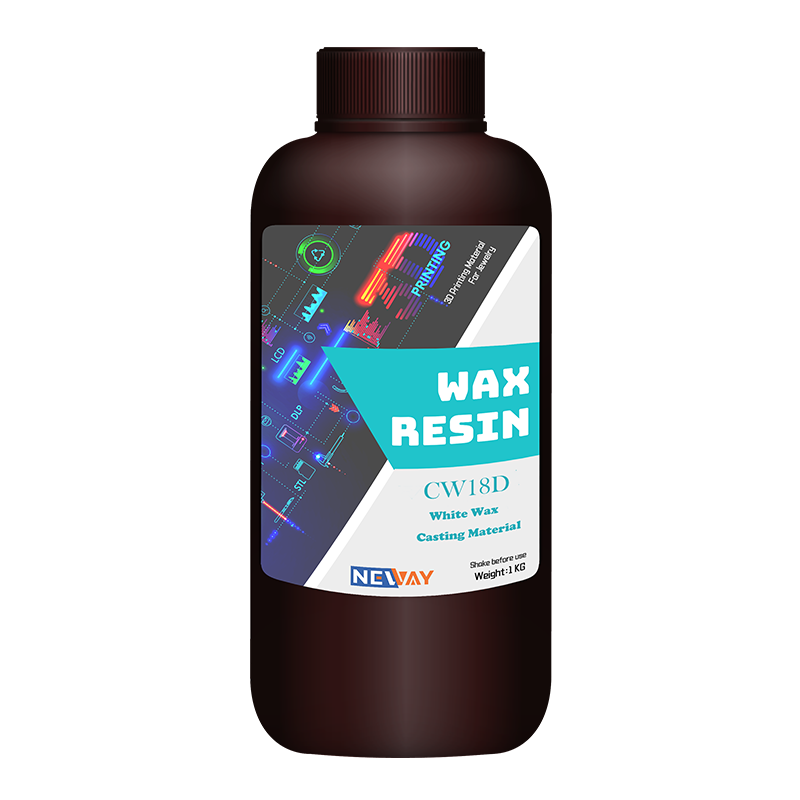
Frequently Asked Questions
Q: What is black wax casting resin?
A: Black wax casting resin is a dark, wax-like photopolymer designed for lost-wax investment casting. It prints sharp jewelry patterns and burns out cleanly in the furnace, leaving little ash on the metal.
Q: How long does black wax casting resin take to cure?
A: After printing, wash the part in isopropyl alcohol, then UV post-cure for 1-5 minutes depending on thickness. Full cure gives the pattern proper handling strength before investing.
Q: Why is it called black wax resin?
A: It behaves like injection wax but is deep black in color. The dark finish shows up support marks and surface texture clearly under light, which is useful for QC before casting.
Q: How do you burn out black wax casting resin?
A: Follow a slow burnout schedule with a gradual temperature ramp and a hold at peak temperature to fully decompose the polymer. Proper burnout prevents residual carbon and casting defects.
Q: What layer height works for black wax casting?
A: Print at 20-50 µm layers for jewelry casting. Finer 20-30 µm layers produce smoother cast surfaces; 50 µm layers are faster for bulk or less detailed pieces.
